A micro drill is a compact tool for drilling and light machining where hand work would simply take too long. Two kinds turn up: mechanical holders with a quick hand drive, which behave like an improved pin vice, and electric micro drills with speed control. In both cases the clamping range is very small, matched to fine bits and to burrs with a slender shank, and neither is intended for anything a workshop drill would be handed. Neither replaces a pin vice; they take over at the point where the number of holes, not their difficulty, is the problem.
The moment there are a lot of holes. A perforated screen, a row of riveted holes, twenty opened gun muzzles on one armour subject — a pin vice can do all of it, but it will cost you an evening. The second reason is hard material: resin, cured two-part putty and metal drill slowly and strenuously by hand.
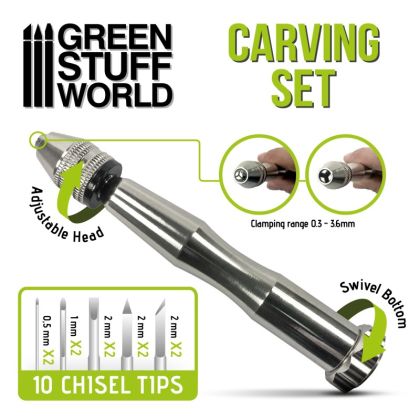
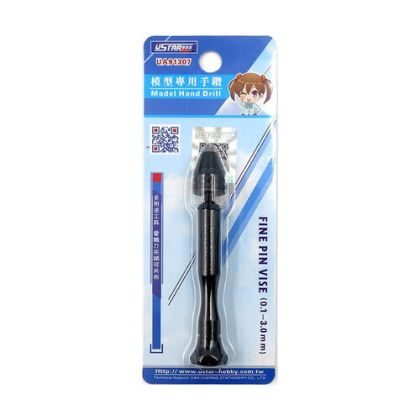
The drive comes from pressing or quickly working the handle, so no power supply is needed and you keep the feel of the cut. They are quiet, light and suited to styrene. Into hard materials they will not get as easily as a powered tool.
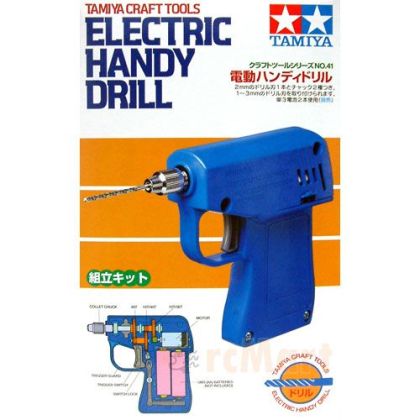
These have a motor and most often speed control, which for modelling is the key specification — high speed melts styrene. They also serve for milling, sanding and polishing, provided the right accessory is fitted.
Check which shanks the tool accepts. Modelling burrs and grinding heads usually have a standardised shank diameter, while fine drill bits are much thinner and need a collet of their own. The accessories live in tools for micro drills.
Always start at the lowest speed and add only what you need. The part must be clamped rather than held in the fingers — a rotating tool can snatch a small component out of your hand. On resin and printing resins wear a respirator and use extraction where you can, because the dust is a health hazard. Help with that is in electric tools.
For a single hole in a thin wall the safer choice remains a hand-turned tool from drilling and milling.